FOR INDUSTRIAL AND LABORATORY RESEARCH USE ONLY. NOT FOR DIRECT HUMAN CONSUMPTION, THERAPEUTIC OR HOUSEHOLD USE.
For industrial manufacturing and laboratory research purposes only.
Product Specifications
| Parameter | Value |
|---|
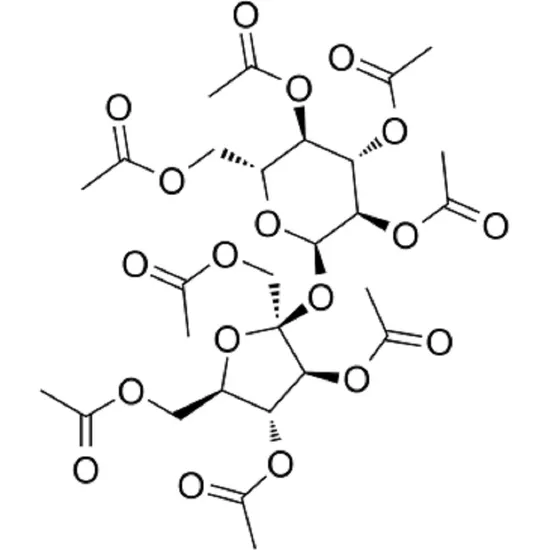
| Product Name | Sucrose Octaacetate |
| CAS Number | 126-14-7 |
| Purity | >99% |
| Purity Degree | 99% |
| State | Solid |
| Molecular Formula | C28H38O19 |
| Melting Point | 82-85 °C(Lit.) |
| Boiling Point | 668.3±55.0 °C at 760 mmHg |
| Transport Package | by Foil - Alum Bag or Paper Drum |
| Specification | 250kg/drum Or 1, 250kg/IBC |
| Origin | Hangzhou |
| HS Code | 2940000000 |
Combat Production Delays with Consistent High Purity Sucrose Octaacetate CAS 126-14-7
We've witnessed countless production disruptions in chemical processing plants – batch-to-batch purity fluctuations causing unexpected副反应, delayed bulk deliveries halting production lines, and inconsistent material quality leading to failed product testing. As a supplier with over a decade of experience serving industrial clients, these challenges aren't just statistics; they're daily obstacles our customers face in maintaining operational efficiency.
A Stable Supply Chain Solution for Industrial Scale Operations
Our High Purity 99% Sucrose Octaacetate CAS 126-14-7 addresses these critical pain points through a vertically integrated supply chain. With large-scale warehousing facilities and established production protocols, we guarantee consistent availability from kilogram to ton-level orders, eliminating the risks of supply interruptions that plague many chemical manufacturers. This stability is why we've become the trusted partner for industrial chemical distributors and processing plants across 50+ countries.
Key Industrial Applications of Sucrose Octaacetate
Sucrose Octaacetate 126-14-7 for Industry serves as a critical intermediate in multiple manufacturing processes. Its unique chemical properties make it valuable in polymer synthesis, specialty coating formulations, and as a processing aid in plastic and rubber manufacturing. The compound's solid state and high purity also render it suitable for controlled-release applications in industrial materials science research, providing consistent performance in laboratory scale studies and full-scale production environments.
Why Purity and Physical Properties Matter in Industrial Use
The 99% purity level of our Sucrose Octaacetate is not merely a technical specification but a critical quality parameter that directly impacts production outcomes. This high purity minimizes impurity-related副反应, ensuring cleaner synthesis processes and reducing waste disposal costs. The well-defined melting point range (82-85°C) guarantees predictable thermal behavior during manufacturing, while the stable solid state allows for precise dosing and handling in automated production lines. These characteristics translate to more consistent finished products and reduced quality control failures, particularly in sensitive coating and polymer applications where material consistency is paramount.
Operational Advantages of Reliable Chemical Sourcing
Choosing a supplier with stringent quality control directly impacts your bottom line. Our High Purity Sucrose Octaacetate reduces production variability, lowering reject rates and rework costs associated with inferior raw materials. Unlike suppliers offering inconsistent quality, our commitment to batch-to-batch uniformity ensures your manufacturing processes remain stable, protecting your production schedules and customer commitments. With our large warehousing capacity and flexible delivery options, you can optimize inventory levels, reducing carrying costs while maintaining production continuity – a critical advantage in today's volatile chemical market.
Our Quality Assurance Commitment
Every batch of Sucrose Octaacetate undergoes comprehensive testing using HPLC and NMR analysis to verify purity and chemical identity. We provide a detailed Certificate of Analysis with each delivery, documenting key parameters including melting point, purity, and physical characteristics. Our production facilities operate under strict quality management systems, ensuring compliance with international industrial chemical standards. In the rare event of non-conformity, our no-questions-asked return policy guarantees prompt resolution, demonstrating our confidence in product consistency and commitment to customer satisfaction.
Certificate of Analysis & Documentation
Each shipment includes a batch-specific Certificate of Analysis (COA) detailing all tested parameters and compliance results. Material Safety Data Sheets (MSDS) are provided with every order, containing comprehensive handling, storage, and safety information. For qualification purposes or detailed technical review, additional analytical data including chromatograms can be made available upon request, supporting your quality control and regulatory compliance requirements.
Storage & Handling
- Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
- Keep away from incompatible materials, food and feed sources.
- Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
- Follow good industrial hygiene practices. Avoid inhalation and skin contact.
- Refer to MSDS for detailed storage and safety instructions.
Streamlined Industrial Procurement Process
Initiate your order by submitting a detailed procurement list specifying required quantities and packaging preferences. Our technical team will confirm availability and provide a comprehensive quotation including delivery timelines. For new applications, we recommend requesting a sample for qualification testing prior to full-scale ordering. Once specifications are confirmed, our standard transaction process ensures efficient order processing, production scheduling, and delivery coordination to meet your production timeline requirements.
Frequently Asked Questions
Q: What is the recommended shelf life for Sucrose Octaacetate when properly stored?
A: When stored in sealed containers under recommended conditions, the product maintains stability for 24 months from the date of manufacture.
Q: Can this product be used in food, pharmaceutical, or cosmetic applications?
A: No. This product is supplied exclusively FOR INDUSTRIAL AND LABORATORY RESEARCH USE ONLY. NOT FOR DIRECT HUMAN CONSUMPTION, THERAPEUTIC OR HOUSEHOLD USE.
What documentation is provided with each shipment?
A: Each delivery includes a batch-specific Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS) as standard documentation.
Q: Are custom packaging options available beyond the standard specifications?
A: Yes, shipping marks can be customized according to customer requirements. For specialized packaging needs, please discuss with our sales team during the quotation process.
Q: How is the purity of your Sucrose Octaacetate verified and guaranteed?
A: Purity is verified through HPLC analysis for each production batch, with results documented in the COA. Our quality control process ensures purity consistently meets or exceeds the 99% specification.
Usage Notice: Supplied exclusively for industrial manufacturing and laboratory research purposes. The buyer is fully responsible for complying with all local laws, regulations and safety requirements for its use.
 Fine Chemical Intermediates


